30 Sept 2026
CO2 Recovery Plant for CO2-rich raw gas streams
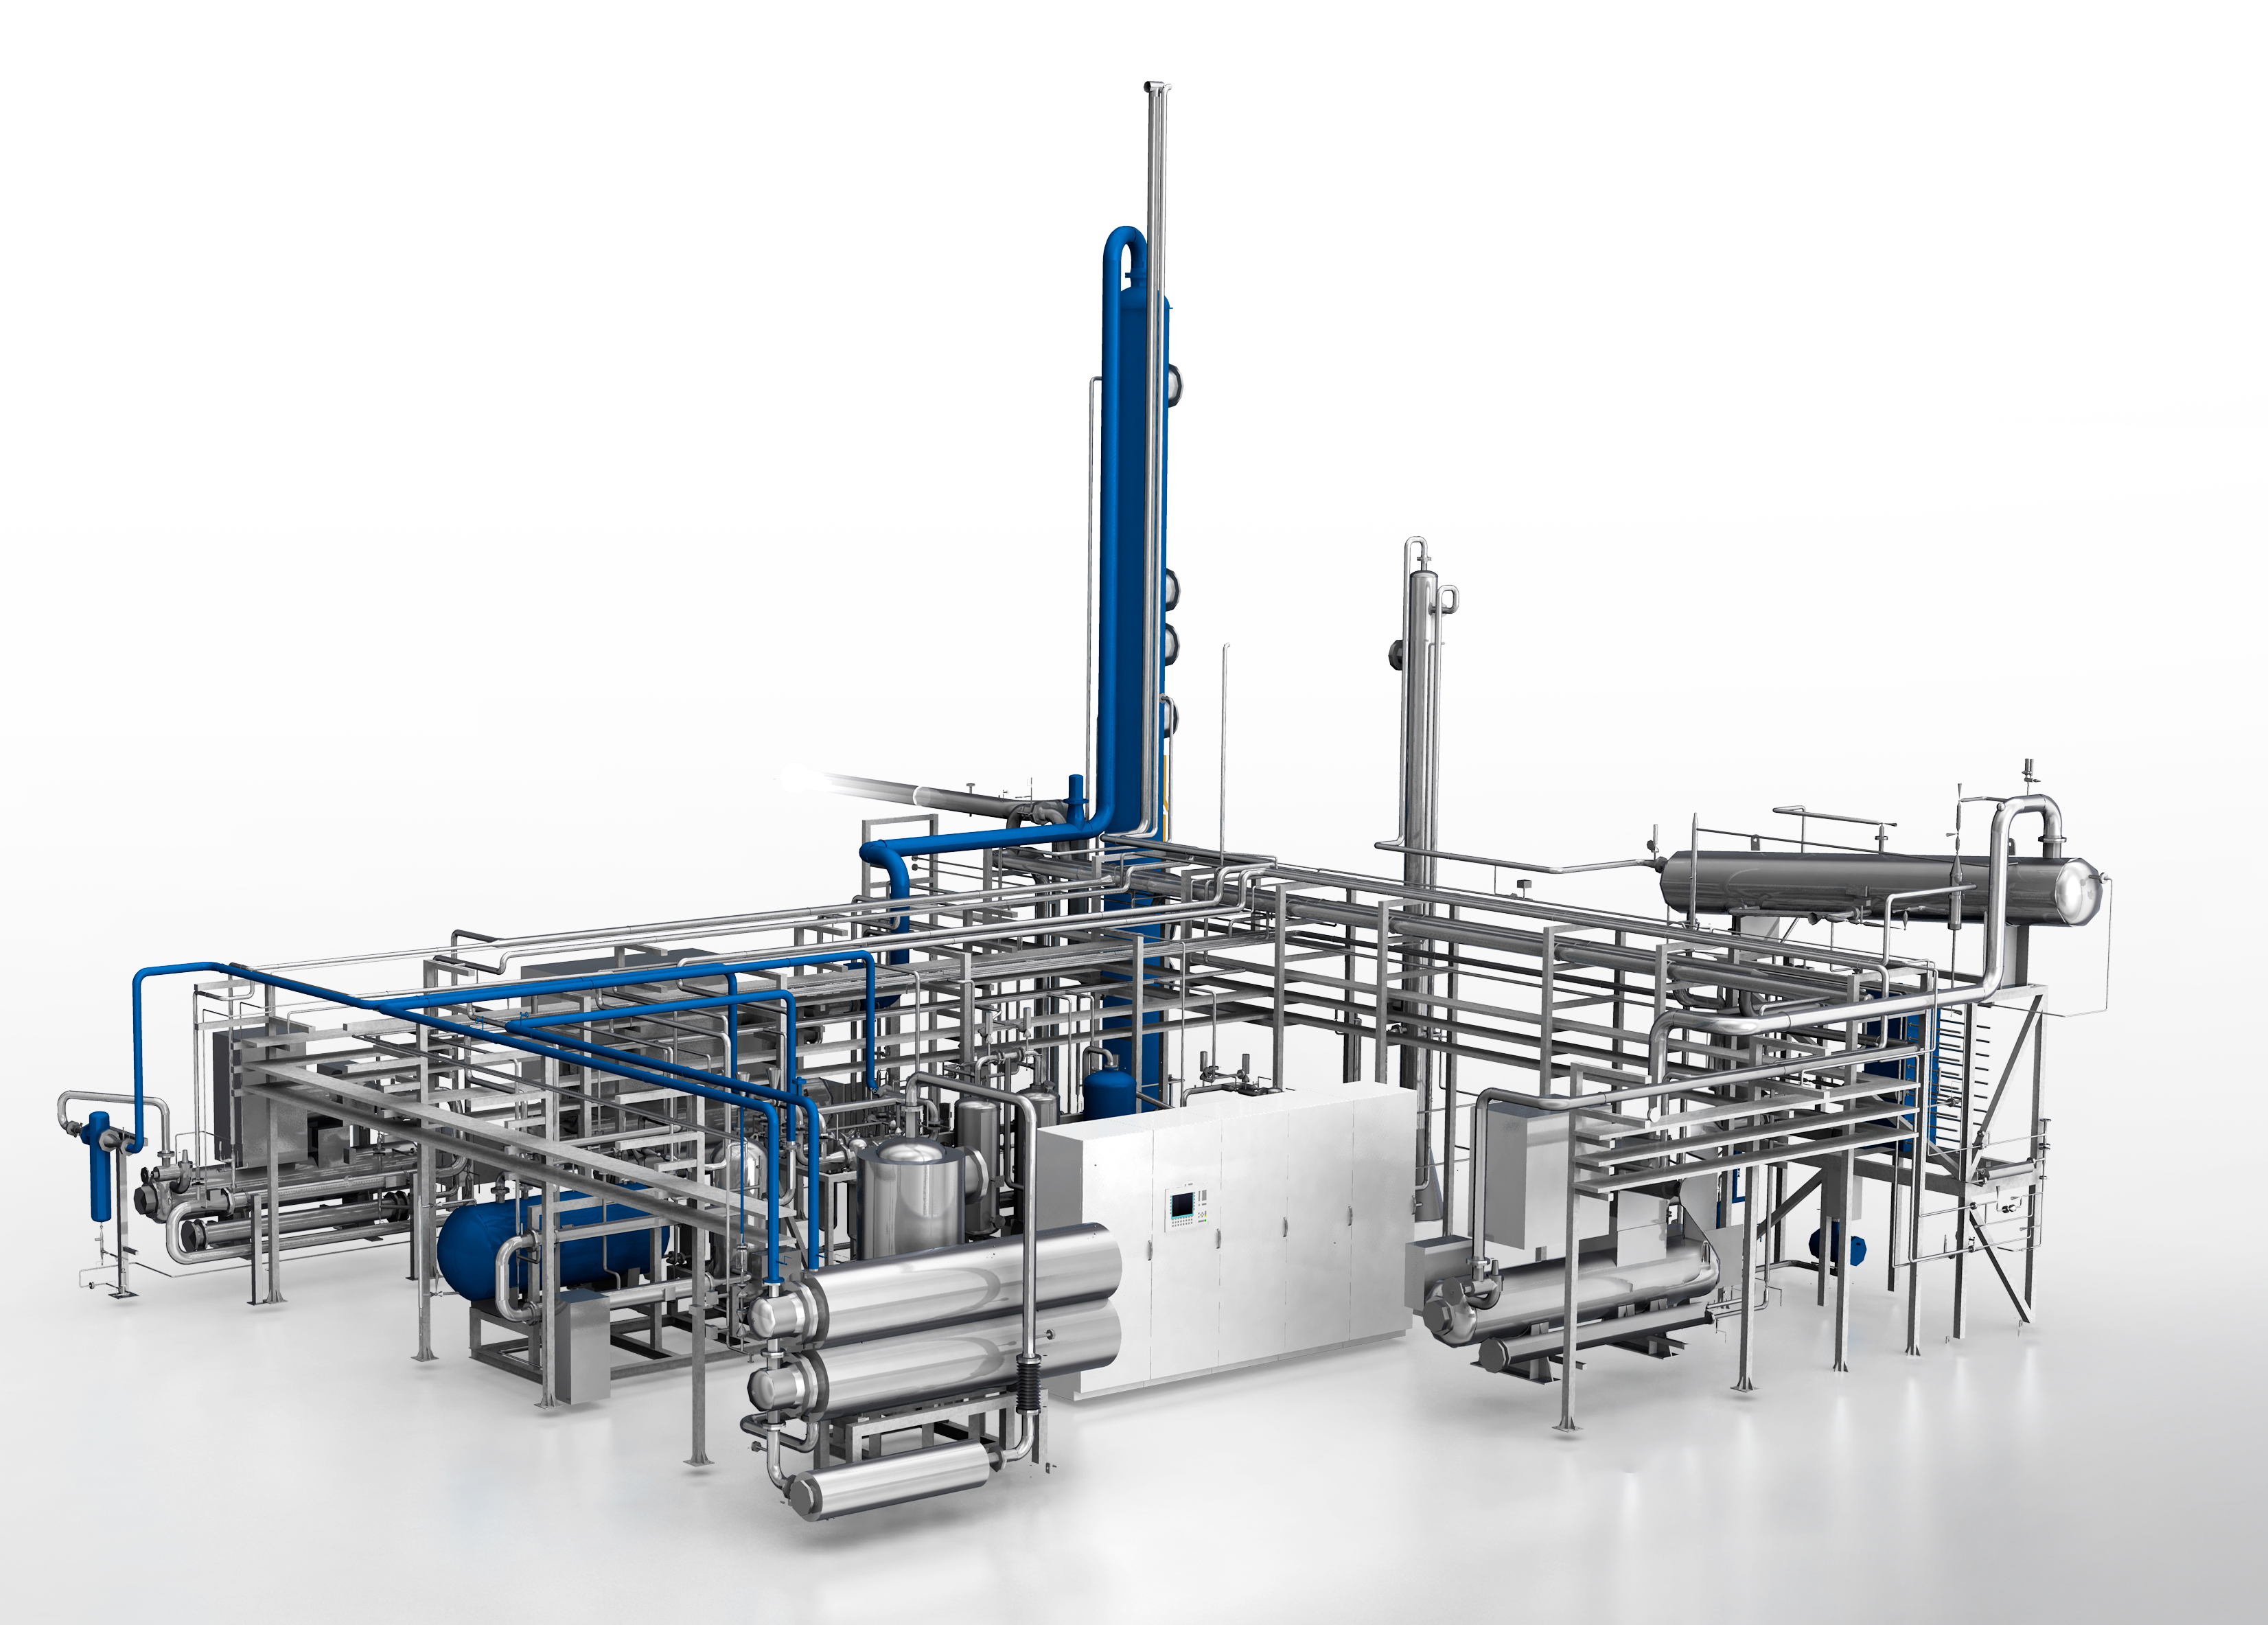
Each RBU is built around a precise understanding of the customer’s feed gas composition, impurity profile, required CO2 quality, operating conditions, and business objectives. By combining standardized process blocks with application-specific engineering, Pentair can tailor each solution to deliver the required CO2 specification and quantity while optimizing CAPEX, OPEX, reliability, and overall lifecycle performance.
Benefits:
♦ High-quality liquid CO2 production
♦ Tailored purification for every feed gas profile
♦ Competitive lifecycle cost performance
♦ Reliable compliance with demanding CO2 specifications
♦ Sustainable long-term operation