INTALOX® ULTRA Random Packing: Maximizing Carbon Capture Performance with Lower Pressure Drop
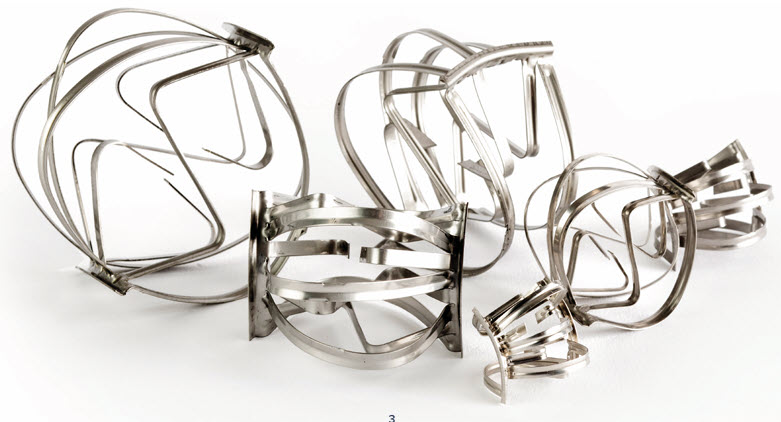
As carbon capture facilities pursue higher CO₂ removal rates while minimizing energy consumption and capital investment, packing selection becomes a critical design decision. INTALOX® ULTRA random packing was developed by Koch-Glitsch to bridge the traditional trade-off between capacity and efficiency, delivering superior performance for gas treating and carbon capture applications.
Built on decades of experience in mass transfer technology, INTALOX® ULTRA features an advanced geometry that maximizes effective surface area while maintaining very low pressure drop. The result is a packing solution that can increase tower capacity by up to 10% while maintaining comparable efficiency to previous high-performance random packing technologies.
For carbon capture and acid gas removal systems, lower pressure drop translates directly into operational benefits. Absorber columns can operate with reduced energy consumption, lower solvent degradation, reduced foaming tendencies, and decreased solvent losses. When combined with INTALOX® high-performance liquid distributors, INTALOX® ULTRA provides predictable and reliable absorption performance for demanding CO₂ capture duties.
Koch-Glitsch has successfully applied INTALOX® ULTRA packing in numerous acid gas removal systems, including amine, hot carbonate, and physical solvent applications. The technology's combination of high capacity, low pressure drop, and reliable performance makes it an ideal solution for the next generation of carbon capture projects seeking maximum CO₂ removal efficiency and improved project economics.